PPA-CF or PA6-CF depends on how humid your workshop gets
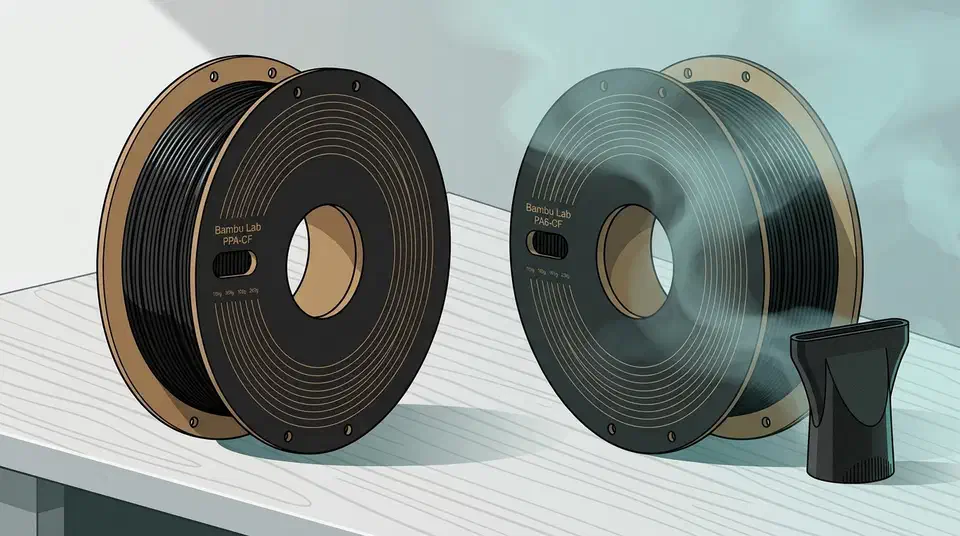
On the spec sheet, PPA-CF is stronger, stiffer and takes more heat. PA6-CF bonds its layers 3.6 times better, though, and water settles the rest: wet PA6-CF sheds a third of its strength while PPA-CF barely moves. Pick by the job the part has to do.
Key Takeaways
- PPA-CF is stronger, stiffer and takes more heat on the spec sheet.
- PA6-CF bonds its layers about 3.6 times better, so parts snap less.
- Humidity decides it: wet PA6-CF loses a third of its strength.
- PPA-CF shrugs off moisture, dropping only about 3 percent when wet.
- PPA-CF needs 100 to 140°C drying that most hobby dryers cannot reach.
What is the real difference between PPA-CF and PA6-CF?
Both are chopped-carbon-fiber nylons from Bambu Lab, and on the shop floor they act almost the same. Each needs an enclosed printer, a hardened-steel or high-flow nozzle, and glue on the plate. Where they differ is chemistry.
PPA stands for polyphthalamide, a high-performance nylon with an aromatic backbone. PA6 is ordinary nylon 6. That aromatic backbone is why PPA-CF resists the water and heat that plain PA6 soaks up. PA6 also turns up in industrial blends such as Stratasys’ PA6/66-GF30-FR, a glass-filled nylon certified for rail interiors.
Bambu’s own carbon-fiber usage guide sorts them by environment. It pitches PPA-CF for near-metal strength and stability in humid, hot air, and PA6-CF for high rigidity in long-term dry use.
On the dry spec sheet, PPA-CF leads on almost every headline: 208 vs 151 MPa flexural strength, 9860 vs 5460 MPa stiffness, and a 227°C heat rating against 186°C. On layer bonding and on wet parts, that ranking flips, and the store page doesn’t lead with it.
Where PPA-CF wins on strength, stiffness and heat
Bambu’s dry-state numbers favor PPA-CF. Its flexural strength reaches 208 MPa against PA6-CF’s 151 MPa, a 38 percent edge, so a PPA-CF bracket takes considerably more bending force before it yields.
The stiffness gap is wider. PPA-CF’s flexural modulus is 9860 MPa, roughly 80 percent higher than PA6-CF’s 5460 MPa. It flexes less under the same load, which is what you want in a jig or a tool that must hold a shape.
PPA-CF also handles more heat, keeping its form up to a 227°C heat-deflection point, 41 degrees past PA6-CF’s 186°C. That margin lets PPA-CF go into engine bays and other spots near heat where PA6-CF would soften.
Bambu’s PPA-CF store page markets it as 48 percent stronger and 102 percent stiffer than PA6-CF. The baseline for that claim is a generic “normal PA6-CF” rated at 141 MPa, weaker than Bambu’s own PA6-CF at 151 MPa. Against Bambu’s own filament, the strength gap is closer to 38 percent.
In-plane impact toughness is close to a tie, 41.7 vs 40.3 KJ/m², so PPA-CF’s lead is in stiffness, strength and heat.
Where PA6-CF wins on layer bonding and forgiveness
Most spec dumps skip the number that favors PA6-CF, because it lives on the Z axis. PA6-CF’s interlayer adhesion, measured as Z impact strength, is 15.5 KJ/m² against PPA-CF’s 4.3 KJ/m². With a 3.6x gap, PA6-CF is far harder to split along its print lines.
Most 3D-printed parts fail at the bond between layers before the plastic itself gives way. When a part takes impact or bending across its layers, a stronger seam often counts for more than better numbers on paper.
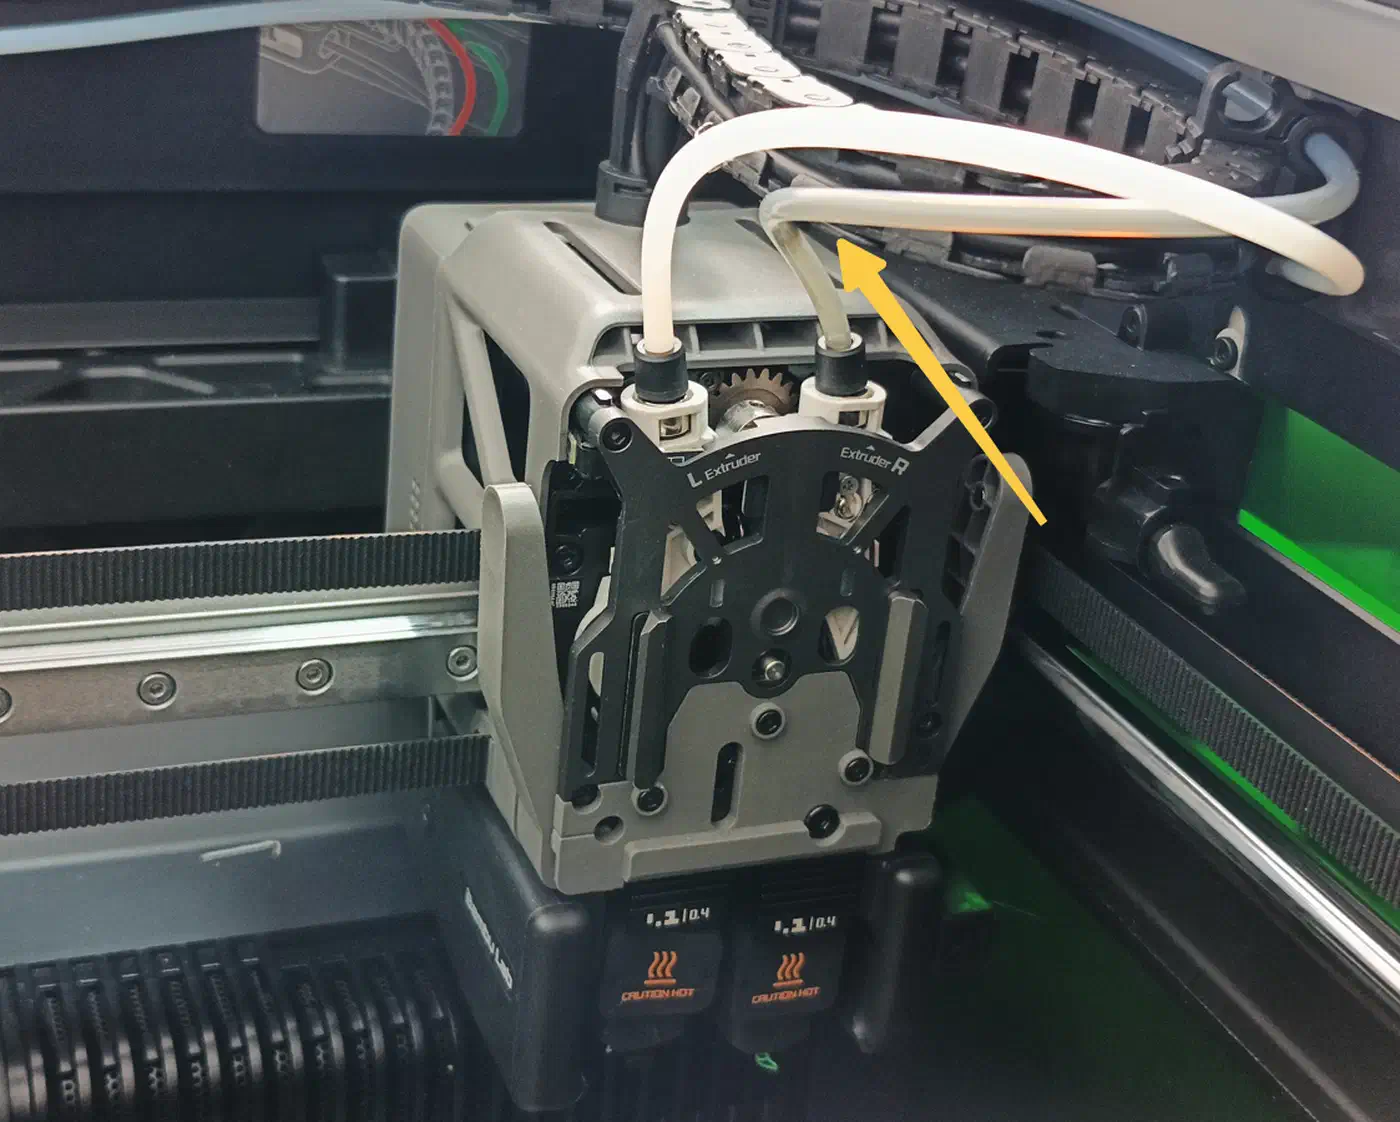
Handling favors PA6-CF too. Bambu describes PET-CF, PPA-CF and PPS-CF as brittle and prone to breakage in the feed path, while PA6-CF is more flexible and needs no extra nozzle securing on the H2D. In practice that means fewer mid-print snaps and cleaner support removal on thin features.
PA6-CF suits functional parts that take impact, snap-fits, near-living hinges, and tall prints where Z strength decides whether the piece survives a drop.
How humidity flips the verdict
Nylon absorbs water from the air, and in service that reverses the comparison.
Humid PA6-CF drops from 151 to 95 MPa strength, down 37 percent, and its stiffness falls from 5460 to 3560 MPa, down 35 percent. Humid PPA-CF barely changes: 208 to 202 MPa strength and 9860 to 9620 MPa stiffness, both under a 3 percent loss.
Water absorption explains the split. At 25°C and 55 percent humidity, PPA-CF saturates at 1.30 percent moisture against Bambu PA6-CF’s 2.35 percent.
The full comparison, dry unless noted:
| Property (dry, XY unless noted) | PPA-CF | PA6-CF |
|---|---|---|
| Flexural strength | 208 MPa | 151 MPa |
| Flexural modulus (stiffness) | 9860 MPa | 5460 MPa |
| Impact toughness (XY) | 41.7 KJ/m² | 40.3 KJ/m² |
| Interlayer bond (Z impact) | 4.3 KJ/m² | 15.5 KJ/m² |
| Heat deflection (0.45 MPa) | 227°C | 186°C |
| Water absorption (25°C, 55% RH) | 1.30% | 2.35% |
| Flexural strength, wet | 202 MPa | 95 MPa |
| Oven drying temperature | 100-140°C | 80°C |
A damp PA6-CF part in service can end up much weaker than a dry PPA-CF part, even though PA6-CF looked competitive on the dry sheet.
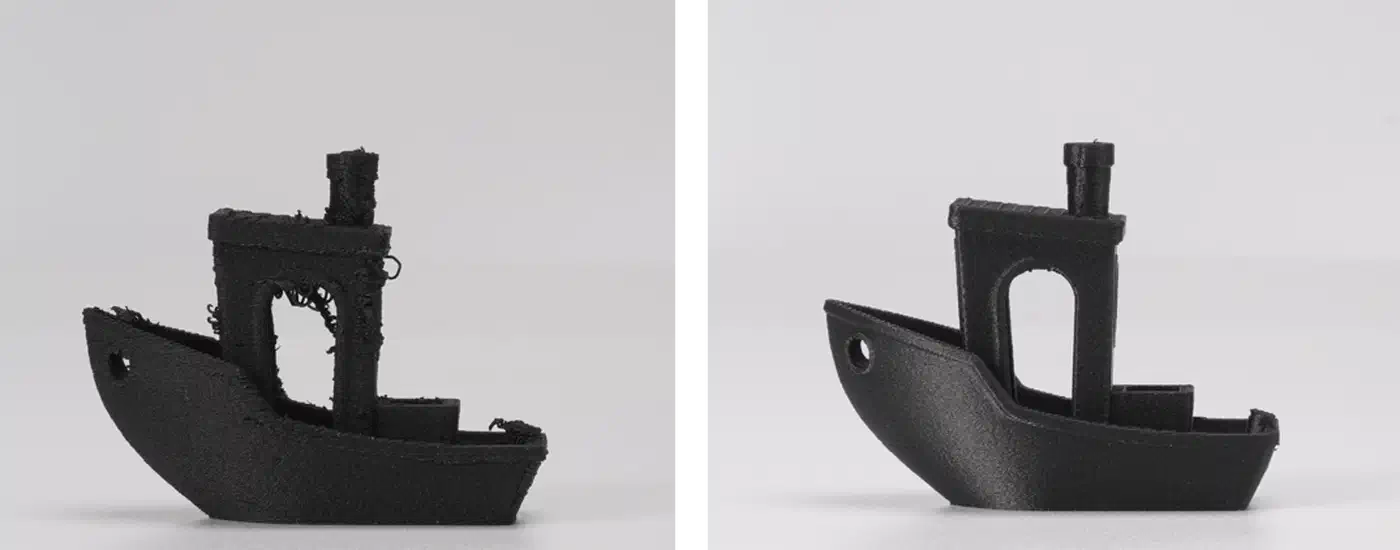
Moisture also shows up at print time. Water inside the filament flashes to steam in the hotend and causes stringing, oozing and a rough surface. Bambu shows this with a boat printed wet and dry, and the wet hull is visibly hairy.
For parts that live in humid air, outdoors or near water, PPA-CF’s stability can outweigh PA6-CF’s layer-bond edge. In climate-controlled dry rooms, PA6-CF’s toughness counts again.
Bambu publishes retained-strength figures rather than a full soak curve, and it does not confirm whether the “humid nylon gets tougher” plasticizer effect seen in some third-party testing applies to its exact PA6-CF blend.
Drying and hardware both filaments demand
The hardware requirements are identical. Drying is where they part, and where buyers ran into trouble.
Both need an enclosed printer, so the P1P and A1 series are out. Only hardened-steel or high-flow nozzles work, with 0.6 mm recommended, glue on the plate is a must, and the AMS series is not compatible.
PA6-CF dries at 80°C for 8 to 12 hours in a convection oven, while PPA-CF needs 100 to 140°C for the same span. Both can dry at 80°C for 12 hours in the AMS HT, which sidesteps the heat problem if you own one.
Consumer filament dryers commonly top out near 70°C, well below PPA-CF’s oven range, and a food oven risks fumes. Buyers ran into this the week PPA-CF launched at USD 99.99.
I just ordered the Sunlu S4 but it only goes to 70 degrees. If that doesn’t do the trick I might have wasted $99.99 on a roll.
Bambu’s support account replied on the same thread with a workaround: a 70°C dryer still works if you run it 18 to 24 hours with the lid cracked so moisture can escape.
One forum user read the spec as 240 to 310°C at the nozzle and a bed of at least 100°C for PPA-CF, and took that to mean X1-class machines. Bambu’s usage guide gives no PPA-CF print-temperature number, so that reading is unofficial. The same thread’s claim of 12 to 18 percent carbon-fiber content comes from users reading the data sheets and is unconfirmed.
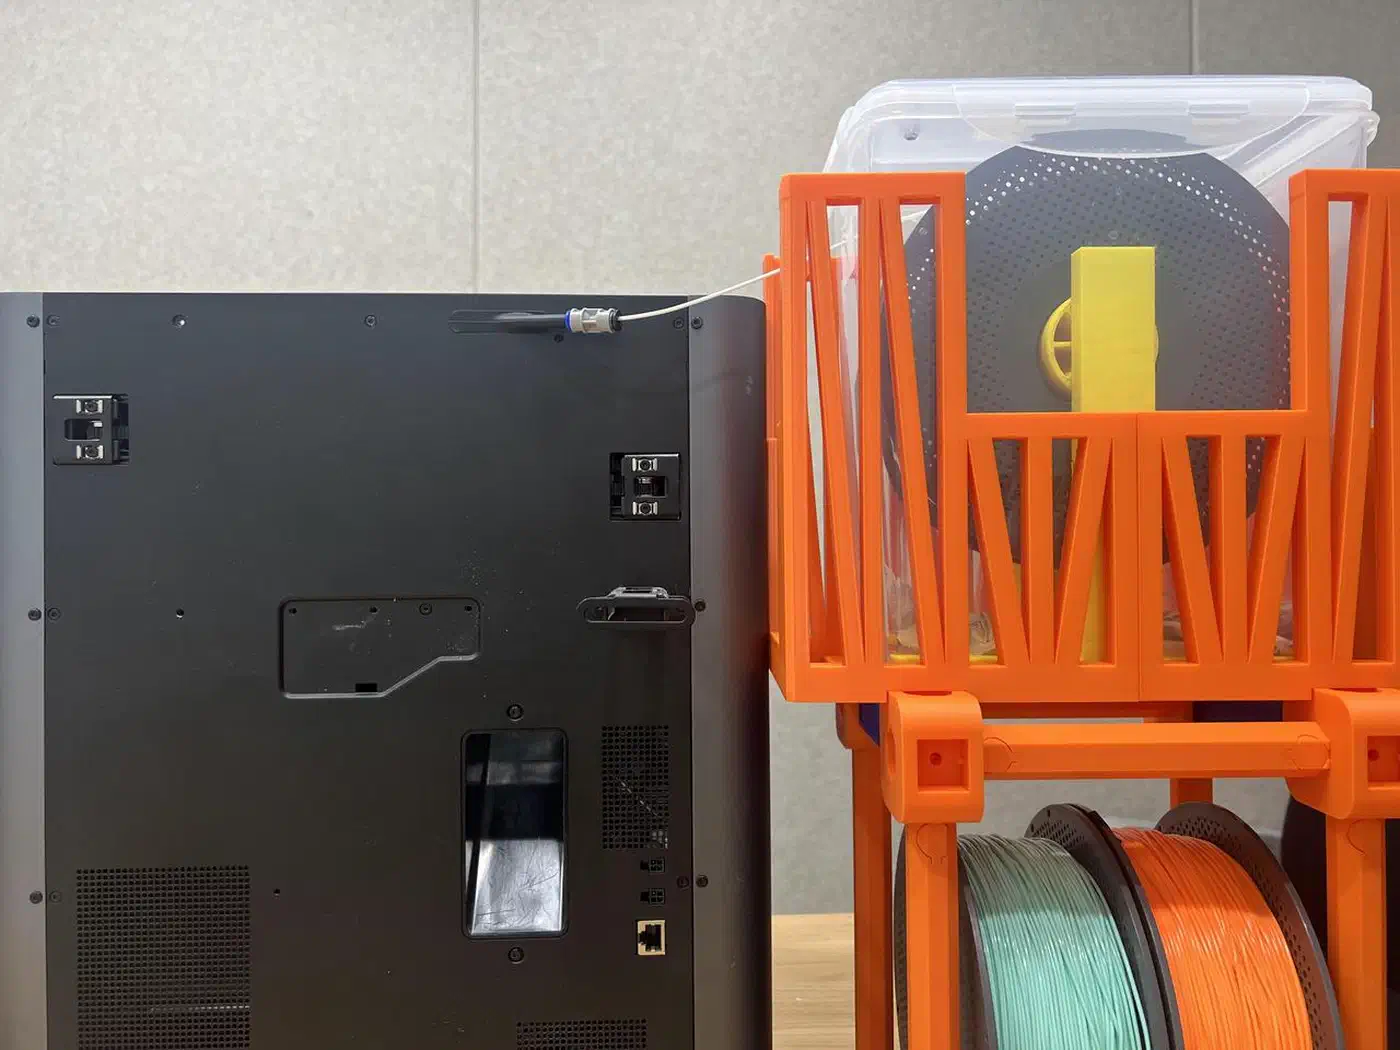
PPA-CF holds up better against moisture in service, but it still absorbs water on the spool. Both need airtight storage with desiccant after every dry.
Which one should you print?
Choose PPA-CF when the part runs hot, lives in humid or wet conditions, or must stay rigid under sustained load, and you own a dryer or oven that reaches past 100°C.
Choose PA6-CF when the part takes impact across its layers, needs to flex rather than shatter, stays in a dry indoor spot, and you want the easier 80°C drying routine.
If the part will ever get damp, lean PPA-CF regardless of the dry-state numbers, because wet PA6-CF hands back most of its advantage. Once moisture is off the table, the rest is a tie-break.