800 hours of carbon fiber leave the Olsson Ruby unworn
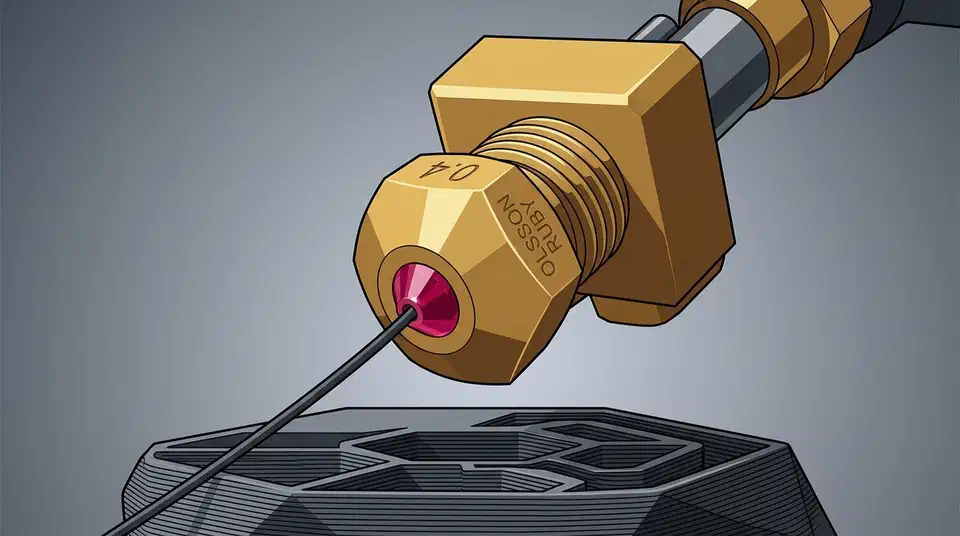
The Olsson Ruby nozzle for carbon fiber came out of an 800-hour test with zero change in orifice diameter. Hardened steel starts slipping at 400 to 600 hours. Only the tip is ruby and the body is brass, so flow behaves like a stock nozzle and your carbon fiber profiles need no retune.
Key Takeaways
- A ruby-tipped nozzle showed zero wear after 800 hours of carbon fiber printing.
- Only the tip is ruby, so flow and temperatures match a plain brass nozzle.
- Ruby rates 9.0 on the Mohs scale, harder than tungsten carbide and close to diamond.
- Above about 15 carbon fiber hours a week, ruby beats replacing steel.
- Ruby is brittle, so one nozzle crash can chip the tip.
Why does carbon fiber filament destroy brass nozzles?
Carbon fiber filament is the material builders reach for when a part has to be stiff and light. The chopped fibers inside it are much harder than brass, though, and they grind away at the orifice every second the printer runs. A tested nozzle roundup from AeroInfill found a 0.4mm brass orifice enlarges measurably within 15 to 20 hours of carbon fiber printing.
Brass rates roughly 3.0 on the Mohs hardness scale. Once the hole widens, dimensions drift and extrusion turns uneven, which brings back the part failures that pushed you toward carbon fiber in the first place.
Wood fill, metal fill, and glow-in-the-dark filaments carry hard particles too. An Ultimaker developer described the worst case:
We had a stainless steel filled material once, that was fun, ruined a brass nozzle before the print could finish.
Among carbon fiber blends, PETG-CF is the gentlest and ABS-CF falls in the middle. PA-CF (nylon carbon fiber) is the harshest, since it pairs heavy fiber loading with high print temperatures.
Why the Olsson Ruby nozzle resists carbon fiber wear
The tip is synthetic single-crystal aluminium oxide, better known as corundum, with about 0.05% chromium mixed in to make it red. A commenter with 20 years in precision ceramic machining spelled that out under the Hackaday article.
Ruby rates Mohs 9.0, above tungsten carbide at 8.5 to 9.0 and just under diamond at 10. No realistic FDM filament is hard enough to cut an orifice made of it.
Diamond would be harder still, but it’s carbon. Carbon can oxidise above roughly 700°C once molten plastic and reactive additives get pushed against it under pressure. Aluminium oxide is chemically inert, so it’s the safer bet inside a hot nozzle.
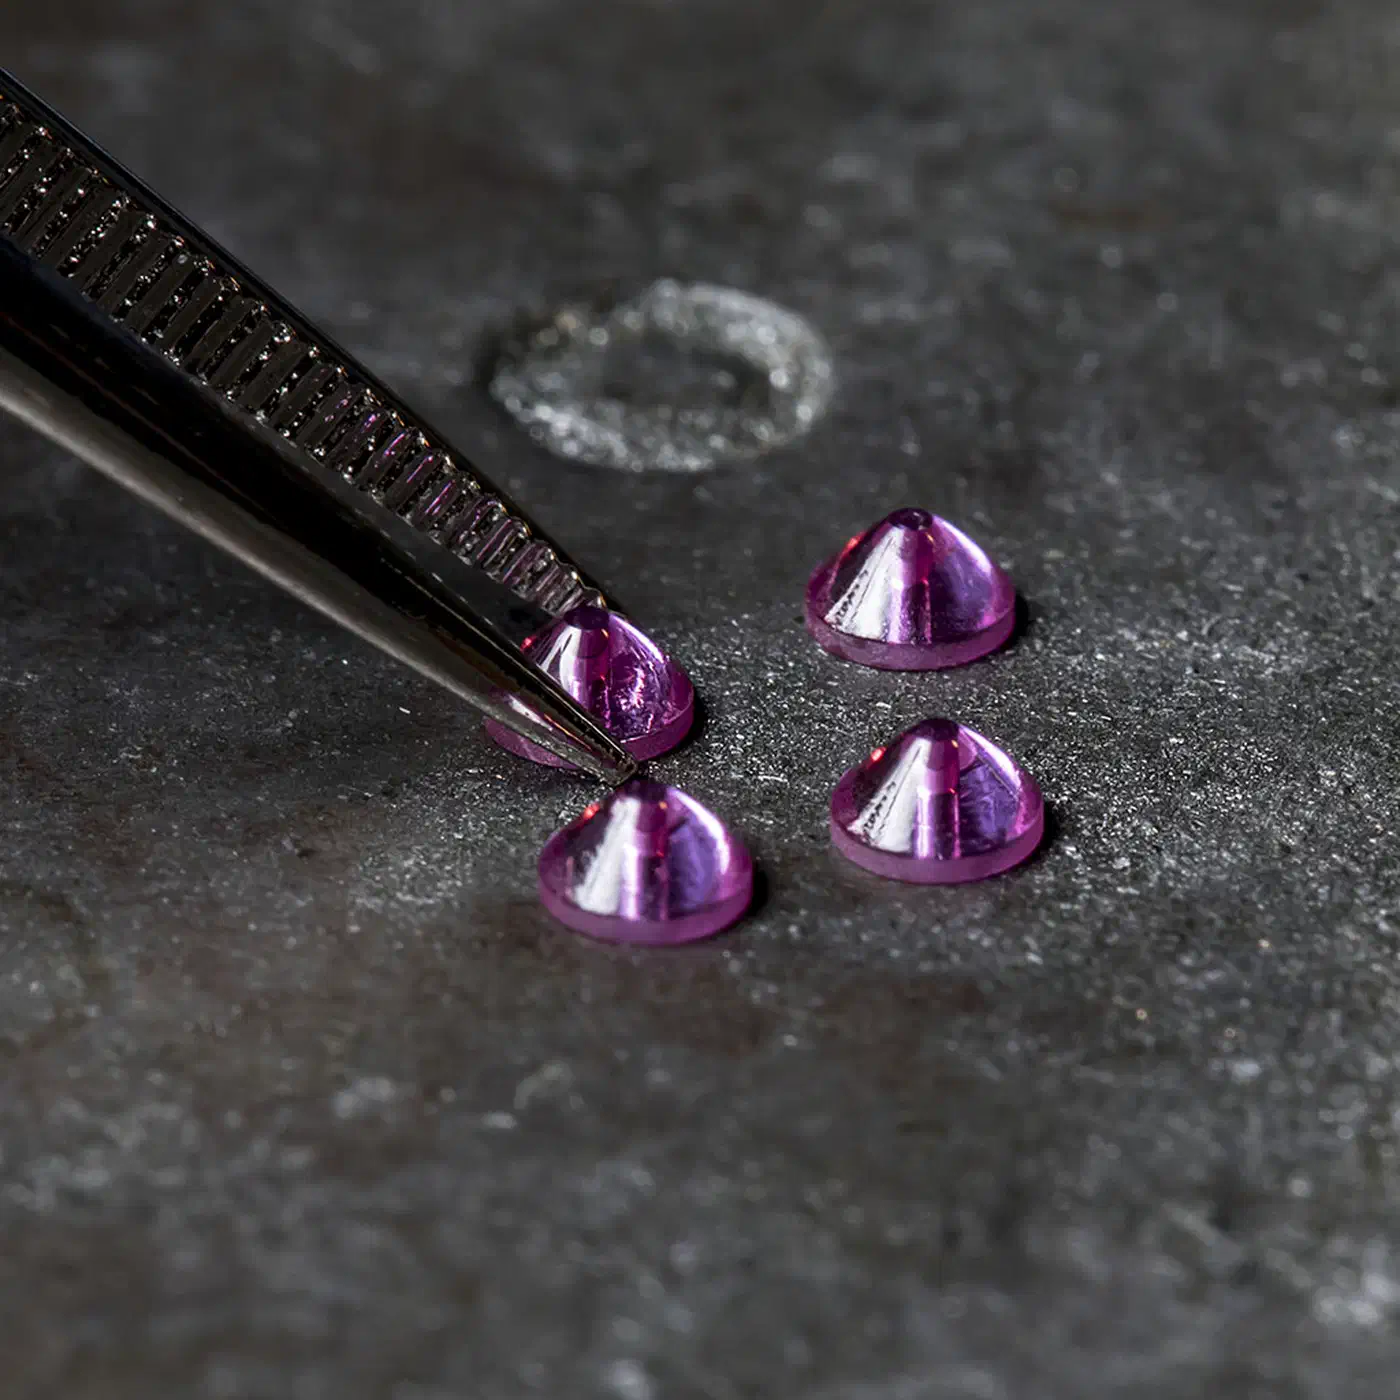
AeroInfill tested across Bambu, Prusa, and Creality machines. After 800 hours of carbon fiber, the Olsson Ruby’s orifice diameter hadn’t changed. The manufacturer documents a service life past 2,000 hours.
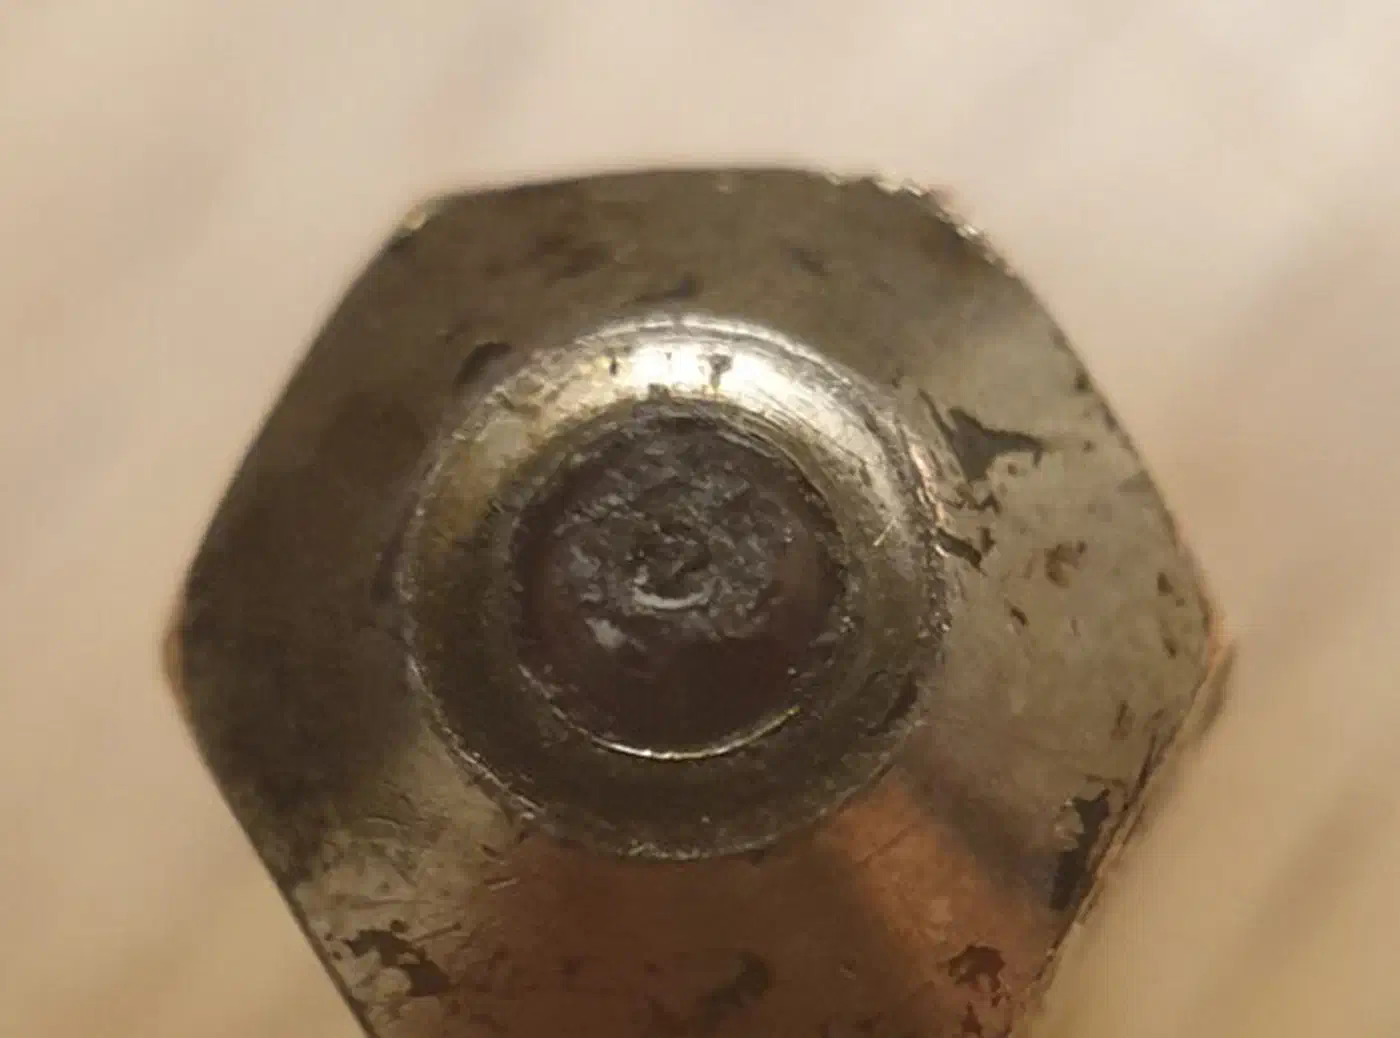
One Trianglelab ruby ran daily for three years, including PEEK at 450°C, before its tip finally went out of shape.
Finally, after 3 years of daily service, my TL Ruby nozzle was decommissioned. It is still working OK, but the Ruby tip has irregular edges. This was by far my most used nozzle and I tested it even with PEEK at 450C. I guess nothing lasts forever, ruby or not.
Ruby vs hardened steel vs tungsten carbide for carbon fiber
Behind the ruby tip, the body is ordinary brass, so heat transfer and flow rate come out effectively identical to a stock brass nozzle.
You can move a dialled-in carbon fiber profile from brass to ruby without touching temperature offsets, retraction or pressure advance. Every other hard nozzle wants a calibration pass first.
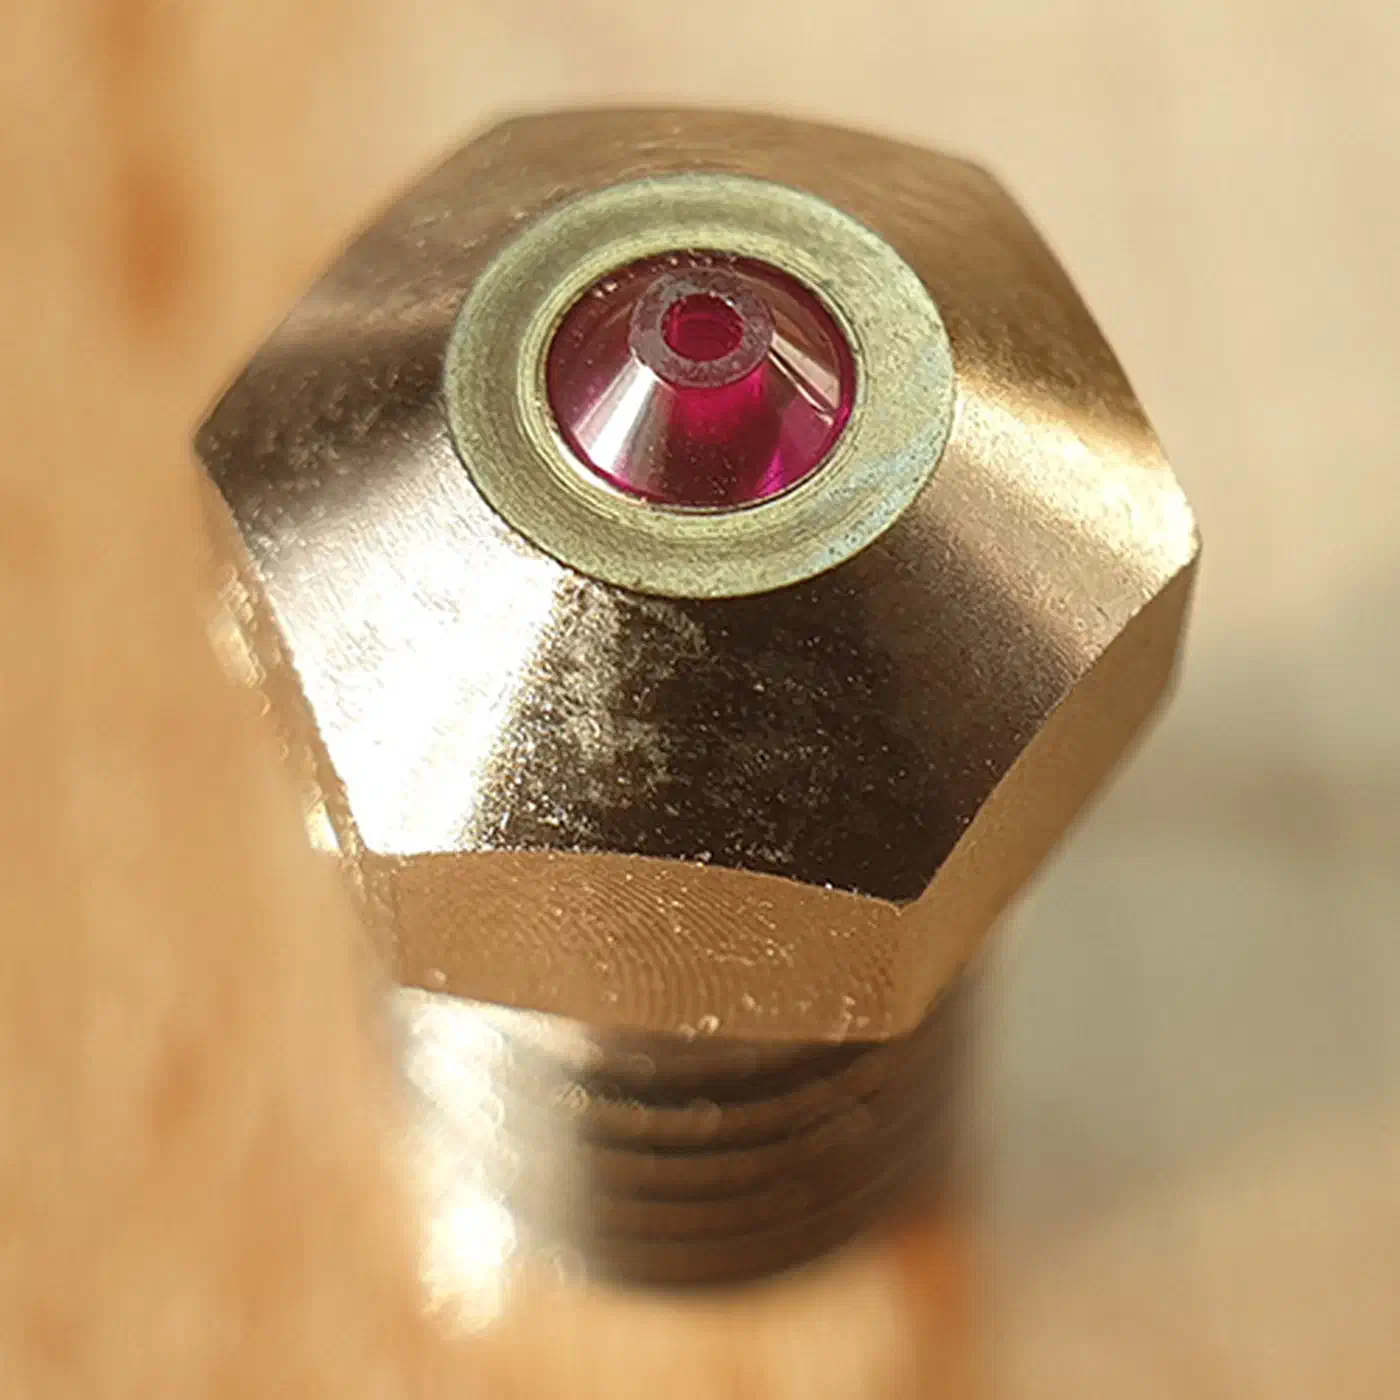
Hardened steel handles PETG-CF for hundreds of hours, and tungsten carbide rivals ruby on hardness for under $20. Both are hard all the way through, so both want a temperature offset. The tungsten body also gives up a little flow ceiling above 200mm/s.
| Nozzle | Price | Tip material | Mohs | Wear rating | Offset vs brass |
|---|---|---|---|---|---|
| Stock brass | ~$3 | Brass | 3.0 | Worn by hour 18 | Baseline |
| E3D Revo hardened steel | ~$25 | Hardened steel | 5.5 | Good | +5 to 10°C |
| Trianglelab tungsten carbide | ~$18 | Tungsten carbide | 8.5 to 9.0 | Very good | +5°C |
| Olsson Ruby | ~$99 | Ruby tip, brass body | 9.0 | Zero wear at 800h | None |
Back in 2017, Ultimaker measured that ruby nozzles of the day needed more force to push the same volume of plastic. Tip geometry is the likely reason. Newer tips flow closer to brass than those early ones did, but anyone chasing peak volumetric flow should test rather than assume.
What the Olsson Ruby costs per hour of carbon fiber
A name-brand ruby nozzle runs about $99 at retail, and the manufacturer’s own listing starts at $90 before VAT. Hardened steel costs roughly $25, and a tungsten carbide tip under $20.
A hardened steel nozzle lasts 400 to 600 hours of heavy carbon fiber before quality slips. Replace it twice a year for five years and you’ve spent about $250. That’s more than one ruby documented past 2,000 hours.
The crossover is near 15 carbon fiber hours a week: hardened steel is the sensible buy below that line, and the ruby wins on cost per hour above it.
The $99 sticker evaporates quickly when you run the cost-per-hour math against hardened steel replacements.
Clone ruby nozzles show up on marketplaces around $25 to $30, while name-brand Olsson and Trianglelab units sell for about $70 to $99. With that spread, a cheap listing isn’t automatically fake.
Trianglelab’s high-temperature version swaps the brass for a plated copper alloy. Copper carries about 10 times the thermal conductivity of steel and three times that of brass. At PEEK and PEI temperatures, that keeps the melt zone steadier.
How do I install a ruby nozzle without chipping the tip?
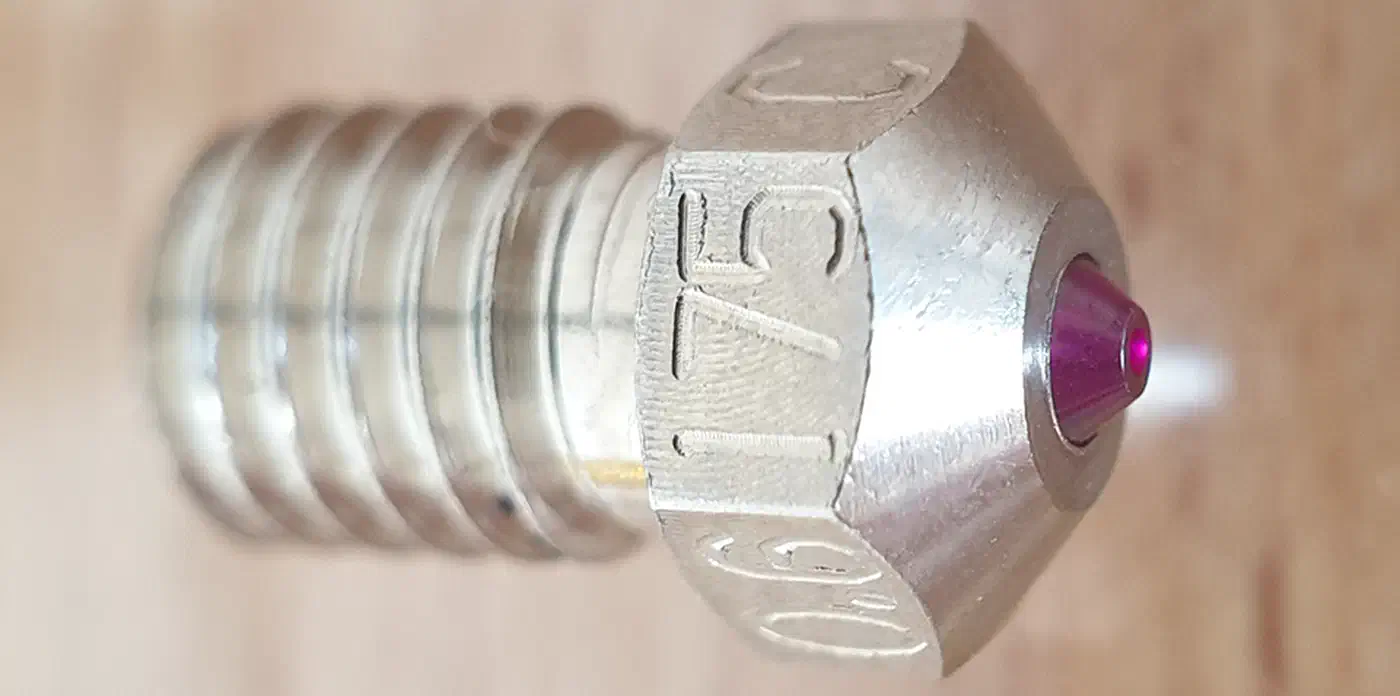
Ruby is brittle as well as hard, and a chipped tip means a dead nozzle. Give the install more care than a $3 brass one gets.
The Olsson instructions call for a torque driver set to 0.5Nm, with 1Nm as the ceiling reported by builders working from the printed instruction sheet. A solid M6 4.6 bolt takes 3.5Nm; drilling a hole through a brass body drops the safe figure sharply.
Always swap the nozzle hot. Cold plastic in the threads acts like glue, and the force needed to break it free is the force that cracks the seat.
A nozzle strike can chip the tip, and no warranty covers a crash. If your first layer is a gamble, fix that before spending $99 on a nozzle.
For sizing, go at least 0.6mm with filled filaments. Smaller orifices clog far more readily on carbon fiber, and a 0.6mm nozzle still prints down to a 0.2mm layer height. Ruby nozzles ship in V6, MK8 (Ender and CR-10), and MK10 threads, so match the format to your hotend before checkout.
Some early three-piece sets shipped with the ruby sleeve only pressed into the body, and a cold pull could back it out. Builder Greg Gallacci solved his by soldering the sleeve in place with lead-free electrical solder, which also improved heat transfer into the tip. A bonded modern unit avoids the problem.
If you print carbon fiber occasionally, hardened steel is plenty and costs a quarter as much. If carbon fiber is what your printer does most weeks, the ruby works out cheaper, and it’s the only hard nozzle that leaves your tuned profiles alone.