Stratasys PA6/66-GF30-FR passes EN 45545 rail fire tests
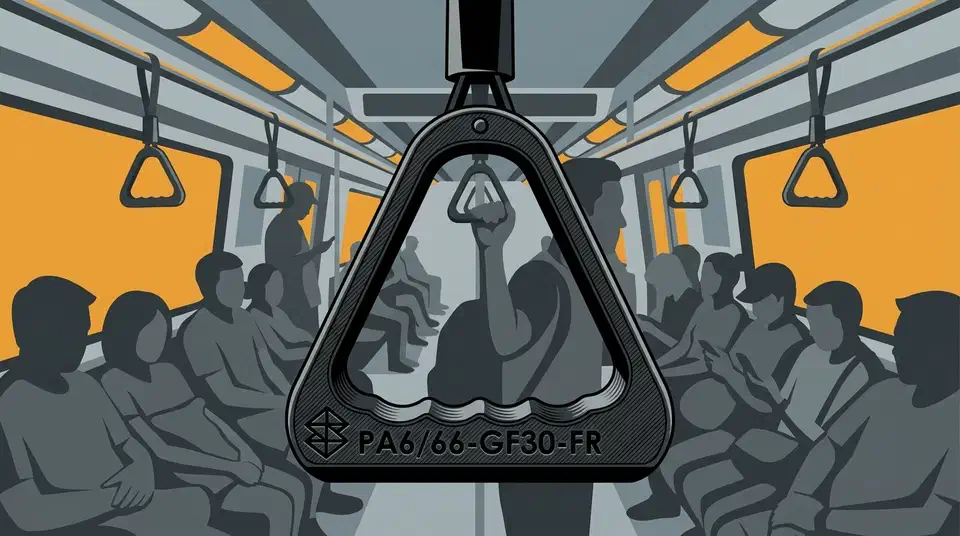
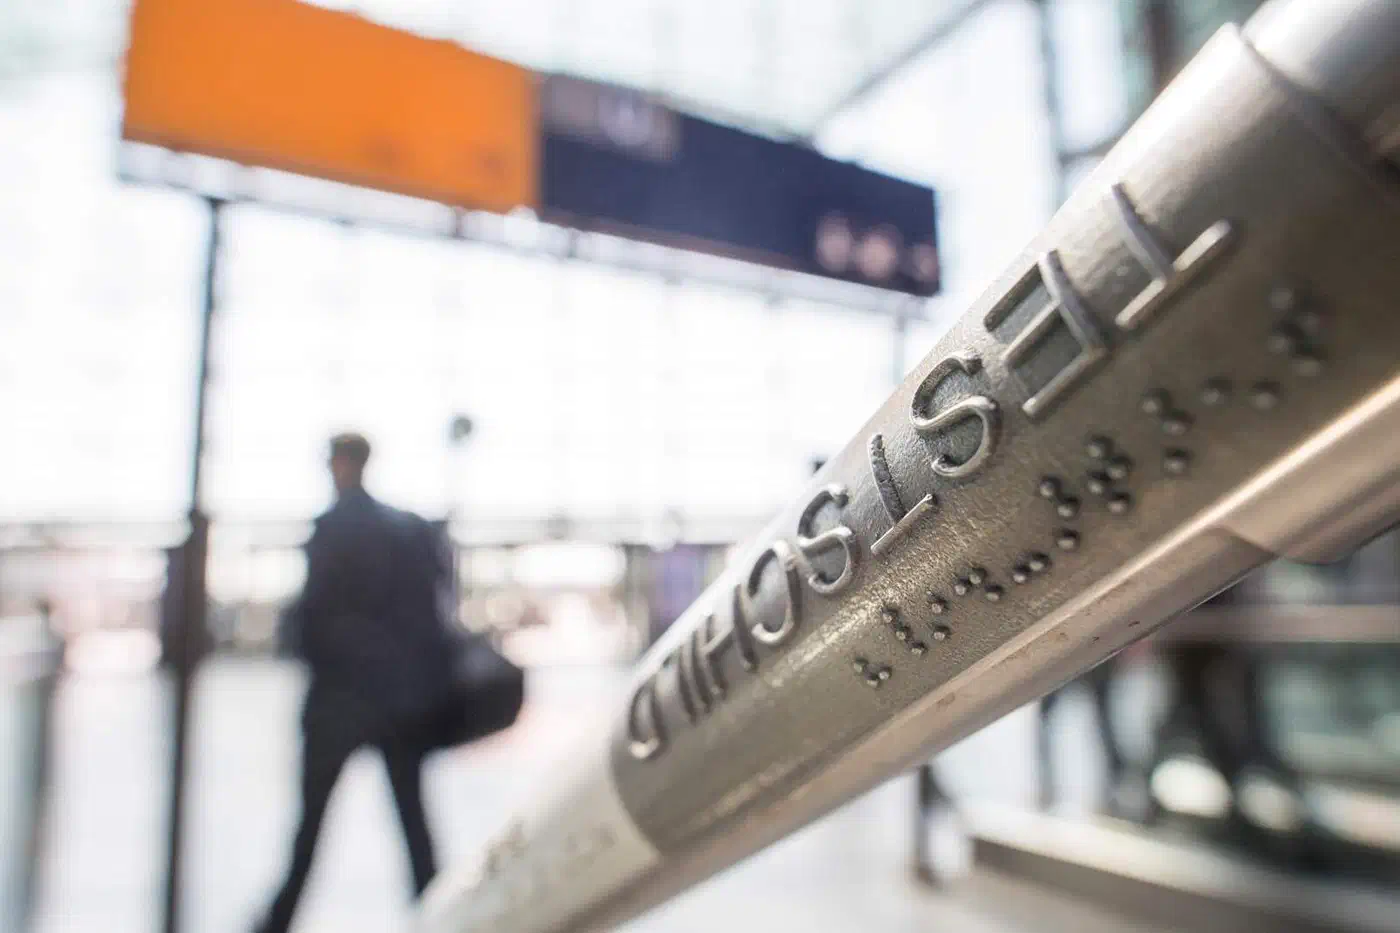
Stratasys’ FDM PA6/66-GF30-FR is a glass-fiber nylon that clears two fire safety rules at once, EN 45545-2 HL2 and FMVSS 302. That certification lets a 3D printed rail handle go on a passenger train in regular service. It’s also a good moment to sort out the three fire tests a printed part can face.
Key Takeaways
- A 3D printed rail handle can now be certified for real service.
- EN 45545-2 HL2 is the test that decides rail use, and UL-94 V0 alone won’t clear it.
- UL-94 V0 means five samples, two flame hits, and no burning drips.
- The nylon is 30% glass fiber and runs on the Fortus 450mc and F900.
- Flame-retardant filaments stink, so you need an enclosed, vented printer.
What is FDM PA6/66-GF30-FR?
FDM PA6/66-GF30-FR is a flame-retardant nylon that Stratasys built for end-use rail and transit parts, with 30% glass fiber added for stiffness.
As reported by 3D Printing Industry, the material clears EN 45545-2 HL2 (requirement sets R22 and R23) and FMVSS 302. That’s what makes a printed part eligible for passenger-facing and structural use, rather than jigs and mockups.
Stratasys also makes two performance claims. It says the nylon beats PC-FR options on stiffness and strength, and comes close to ULTEM 9085. Both come from the vendor, with no independent test data published yet, so treat them as marketing until someone measures them.
The material works with SUP4050B breakaway support, so you snap the support off instead of dissolving it and waiting. It runs only on the Fortus 450mc and F900 industrial systems, so you need one of those printers to use it at all.
Why EN 45545-2 HL2 decides which rail parts can be printed
EN 45545-2 is Europe’s fire safety standard for rail. It decides whether a part is allowed on a train at all. The printers could already make these parts, but without a certified material, additive manufacturing stays in prototyping.
The standard sorts parts two ways. First, by requirement set, the R numbers, where R22 and R23 bundle limits for oxygen index, smoke density, and smoke toxicity. Second, by hazard level, from HL1 to HL3. The level climbs with how hard it is to escape the vehicle. HL1 covers easy-evacuation cases, HL2 covers common passenger vehicles, and HL3 is the strictest tier, for sleeper cars and underground lines.
Clearing HL2 for R22/R23 doesn’t approve the material for every rail use. A part certified at HL2 isn’t automatically cleared for an underground HL3 route, so check the hazard level as well as the standard number.
FMVSS 302 is the separate US rule. It’s a horizontal burn-rate test for road vehicle interiors and doesn’t apply to US railcars, so the pair gets one spool into European trains and US vehicle interiors.
Deutsche Bahn already prints tens of thousands of replacement parts, and in 2023 it certified Essentium’s HSE printer with flame-retardant thermoplastics. The Mobility goes Additive network has since pulled Deutsche Bahn, Austria’s ÖBB, Italy’s Trenitalia, and Swedish railways under one agreement to align how they adopt it. For Alstom, the appeal is a workflow it can certify. Its 3D printing program manager, Lorenzo Gasparoni, said the material supports reliable, repeatable production of qualified spare parts, with easy support removal.
What does UL-94 V0 require?
Almost every flame-retardant filament listing says “UL-94 V0” and almost none explain the test. Per the 3DTrcek product documentation, the test uses five standard samples held vertically, each exposed to an open flame twice for ten seconds.
To pass V0, a material has to clear four conditions:
- Each sample stops burning within 10 seconds after each flame.
- Total burning and glowing across all five samples stays under 50 seconds.
- No flaming drip lights the cotton indicator placed underneath.
- Glowing lasts no longer than 30 seconds after the second flame.
People tend to skip the dripping clause, but a material can self-extinguish and still fail if one burning drop lights the cotton and carries the fire down. Halogen-free chemistry is the norm now, which helps with smoke and toxicity as well as the flame.
UL-94 V0 is a bench test on a small coupon. EN 45545-2 adds smoke density and toxicity limits tuned to the hazard level, so a V0 filament isn’t automatically an HL2 part.
| Test | What it checks | Sample | Pass condition |
|---|---|---|---|
| UL-94 V0 | self-extinguishing of a material coupon | five vertical bars | flame out within 10 s per hit, no drips that light cotton |
| FMVSS 302 | horizontal burn rate of interior parts | horizontal strip | burn rate stays under the set limit |
| EN 45545-2 HL2 | flame, smoke density, and smoke toxicity | varies by part | meets the R-set limits for the hazard level |
The flame-retardant filaments you can print without a Fortus
Most readers will never touch an F900. The 3Dnatives survey of flame-retardant materials lists several other fire-safe options, though they vary widely in what they’re certified to.
| Material | Form | Fire rating it names | Printer it needs |
|---|---|---|---|
| Nanovia PA Rail | nylon plus ceramic filament | unnamed non-flammability standards | high-temp FDM |
| Spectrum PA6 CS20 FR V0 | ceramic-filled nylon filament | EN 45545 and UL-94 V0 | high-temp FDM |
| 3DXTech Fire FR-ABS | ABS filament | UL-94 V0 | enclosed FDM |
| PEEK / PEKK / PEI (ULTEM 9085) | high-performance filament | inherently FR, ULTEM 9085 at UL-94 V0 | high-temp FDM |
| Cubicure Evolution FR | resin | UL-94 V0 (first of its kind) | Hot Lithography |
| PA 2210 FR | powder | UL Blue Card | SLS |
Several of these hold UL-94 V0, and only some name EN 45545, so before you trust one for a rail part, get the vendor’s paperwork for the hazard level you need. The inherently flame-retardant high-performers (PEEK, PEKK, PEI, PVDF, and PPSU) need no additives, but each needs a high-temperature machine, which is what keeps them out of most home shops.
What flame-retardant filament costs you at the printer
Fire safety costs you some printability. 3DTrcek publishes print settings for its ABS FR V0, measured on a Bambu Lab P1S with a 0.4 mm nozzle and a textured PEI plate.
| Setting | Value |
|---|---|
| Nozzle temperature | 240-260°C, 270°C first layer |
| Bed temperature | 80-100°C |
| Volumetric flow | about 18 mm³/s |
| Retraction | 0.8 mm at 30 mm/s |
| Drying | 60°C for 4 to 8 hours |
FR ABS gives off strong, unpleasant fumes, and the vendor flatly advises against open-frame printers. At minimum you want an enclosed chamber in a well-ventilated room, ideally with filtration too. You also want an all-metal hotend for the temperatures involved.
FR ABS warps less than plain ABS but can still lift off the plate, so use a brim and design rounded corners to spread the shrinkage load. Post-processing keeps normal ABS habits, like acetone smoothing and sanding. Heat resistance is about 83°C.
Flame-retardant parts on a hobby printer are realistic: if you can enclose and vent the printer, you can make self-extinguishing parts at home. Certified rail parts still come off an industrial machine.