PA12-CF catches up to PA6-CF once humidity soaks in
In a PA6-CF vs PA12-CF test, the spec-sheet winner and the shelf winner turn out to be different filaments. Fresh off the bed, PA6-CF hits 140 MPa tensile and bends about 40% less than PA12-CF. Then room humidity drops it to 56% of that strength, while PA12-CF barely moves.
Key Takeaways
- Fresh off the bed, PA6-CF is far stronger and about 60% stiffer than PA12-CF.
- Humidity takes back nearly half of that strength within days.
- PA12-CF soaks up a fraction of the water and barely changes.
- Wet PA6-CF gets much tougher, soaking up over half the impact hammer’s energy.
- PA6-CF creeps under constant load unless you anneal it 8 hours at 110°C.
What is the difference between PA6-CF and PA12-CF?
PA is short for polyamide, the material DuPont sold under the name nylon. The number counts the carbon atoms in the building block, so PA6 has six and PA12 has twelve. Both come here with chopped carbon fiber mixed in, which is what the CF marks.
The practical split is water. Filament maker 3DXTech rates PA6-CF at 3 to 9% moisture uptake by weight against under 1% for PA12-CF, and in CNC Kitchen’s head-to-head test the conditioned PA6 bars reached about 3% while PA12 held near 0.7%. That single gap drives almost every result that follows.
PA6 is also 10 to 20% heavier than PA12, and a spool usually costs less. PA12 costs a little more and behaves more predictably.
Chopped fiber cuts thermal expansion and shrinkage, so fiber-filled nylon prints close to as easily as PLA while plain nylon warps. AON3D’s explainer on chopped carbon fiber walks through that mechanism.
Fiber loading decides how strong a CF nylon gets. In AON3D’s datasheet table, an unfilled PA6 copolymer rates 55 MPa and 1.9 GPa, while a 35% carbon-fiber grade reaches 88 MPa and 10.6 GPa. Those are industrial-machine datasheet numbers from mixed vendors, so expect desktop filament to follow the trend without matching the figures.
The dry numbers, where PA6-CF wins everything
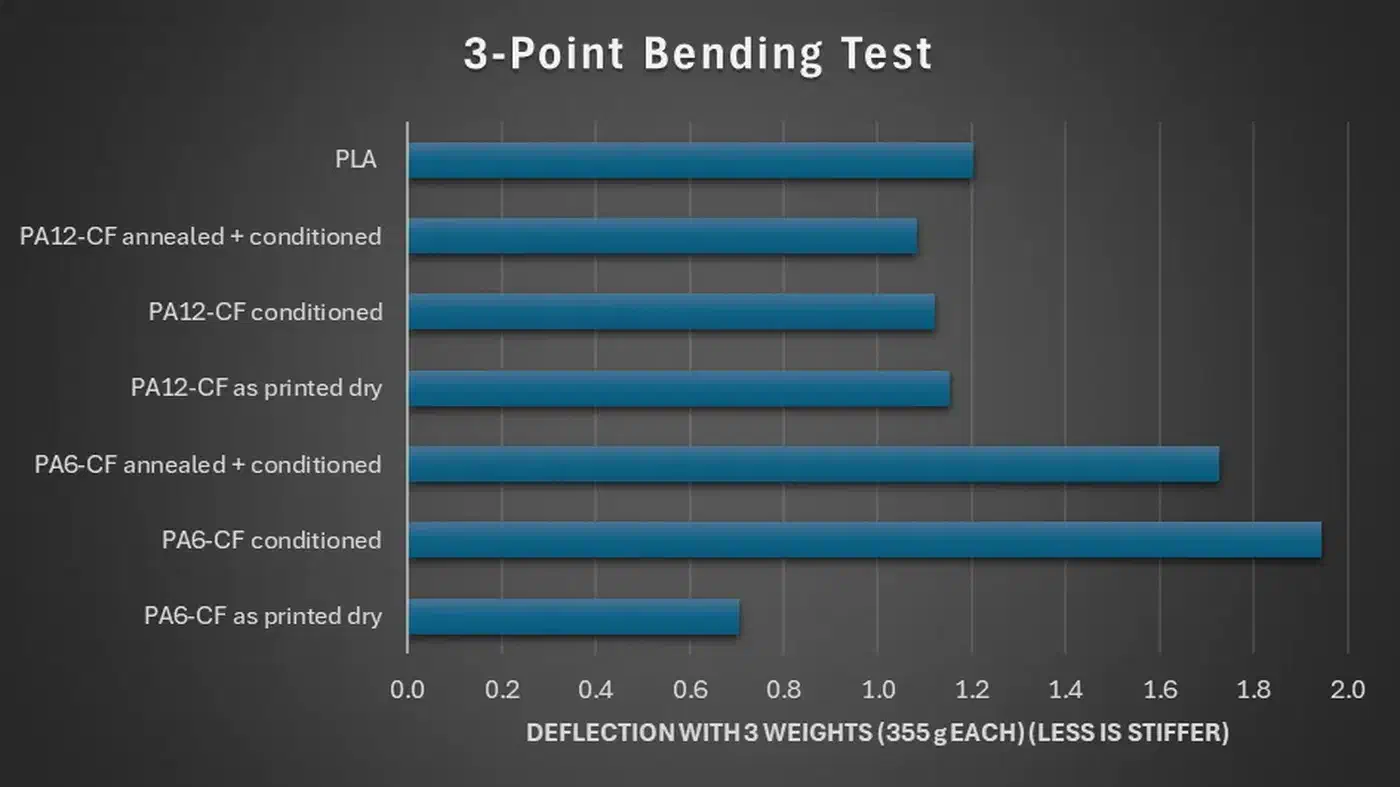
Load three identical bars the same way and the stiffness gap shows up fast. PLA flexed 1.2 mm, SUNLU’s CF-PA12 flexed 1.15 mm, and CF-PA6 flexed only 0.7 mm. Less deflection means more stiffness, so PA6-CF came out about 1.6 to 1.7 times as rigid as either of the others.
The tensile numbers favored PA6-CF too. Printed flat, it broke at 140 MPa, and it split at a second point, so the true figure may be higher. SUNLU’s datasheet claims 170 MPa. Either way, that is two to three times stronger than most common printing plastics.
PA12-CF still broke near 120 MPa, which works out to about 90 kg of load on a small coupon.
Both grades take heat well, and PA6-CF leads here too. PA12-CF softened at 160°C and failed at 170°C. PA6-CF held its shape until 195°C and failed at 205°C. Annealing moved neither number, so 205°C is what PA6-CF gives you straight off the bed.
What moisture does to PA6-CF and PA12-CF
The samples spent three days in a sealed box over saturated table salt at about 75% humidity, inside a 35°C oven, then equilibrated for at least a day. That left PA6 near 3% moisture and PA12 around 0.7%.
Conditioned PA6-CF lost its strength lead, holding just 56% of its dry value, which drops it below conditioned PA12-CF. PA12-CF lost about 15% without annealing, and about 10% when annealed first.
Stiffness fell even harder. The conditioned PA6-CF bar bent almost 2 mm where the dry bar bent 0.7 mm, roughly a third of the original stiffness. Annealing first helped, yet the annealed and conditioned part still kept only 41%. PA12-CF’s bending stayed inside measurement tolerance, and its annealed samples came out slightly stiffer from higher crystallinity.
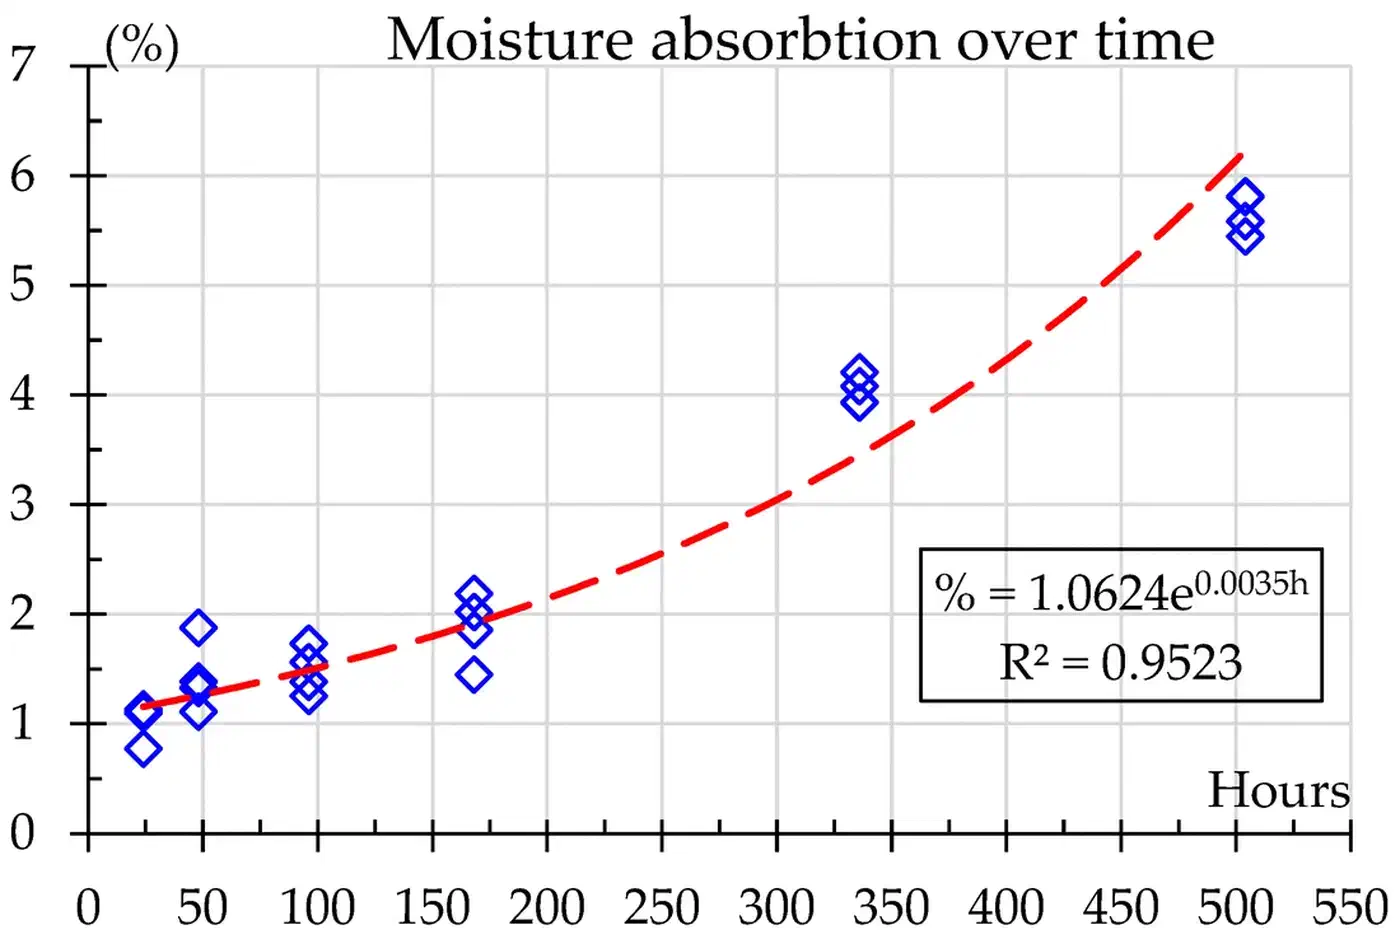
A peer-reviewed test agrees. In a 2026 study in the journal Polymers, Reyes-Flores and colleagues conditioned printed PA6 carbon-fiber bars at a gentler 50% humidity and still logged a 5.6% mass gain over three weeks, with tensile strength and stiffness both drifting down and an infrared scan tracing the loss to water breaking the polymer’s amide bonds. The exposure was milder and the drop smaller, but water softened PA6 the same way.
Layer adhesion followed the moisture. It was barely touched on PA12-CF and clearly reduced on PA6-CF. The carbon fiber only reinforces in the print plane, so it does nothing between the layers.
Water does bring one benefit, because it plasticizes polyamide. Dry PA6-CF already soaked up 15% of the impact hammer’s energy, and the conditioned samples more than tripled that to over 50%, which the test puts in polycarbonate territory. PA12-CF gained a little toughness but never came close. Moisture trades PA6-CF’s strength and stiffness for toughness. Which side of that trade you want depends on whether your part is a bracket or a bumper.
Creep is the main reason to anneal PA6-CF
Creep is slow, permanent deformation under a steady load well inside the elastic range. Nothing overloads; the part just flows away over time.
The bolt test copied a real failure. M4 bolts were torqued to 0.8 Nm through printed blocks, about 50% of the material’s tensile strength, then re-tightened and measured daily for a week.
Un-annealed PA6-CF needed re-torquing almost every day. PA12-CF needed one re-torque after half a week, about the same as PLA and ASA. On PA6-CF, creep shows up long before moisture does.
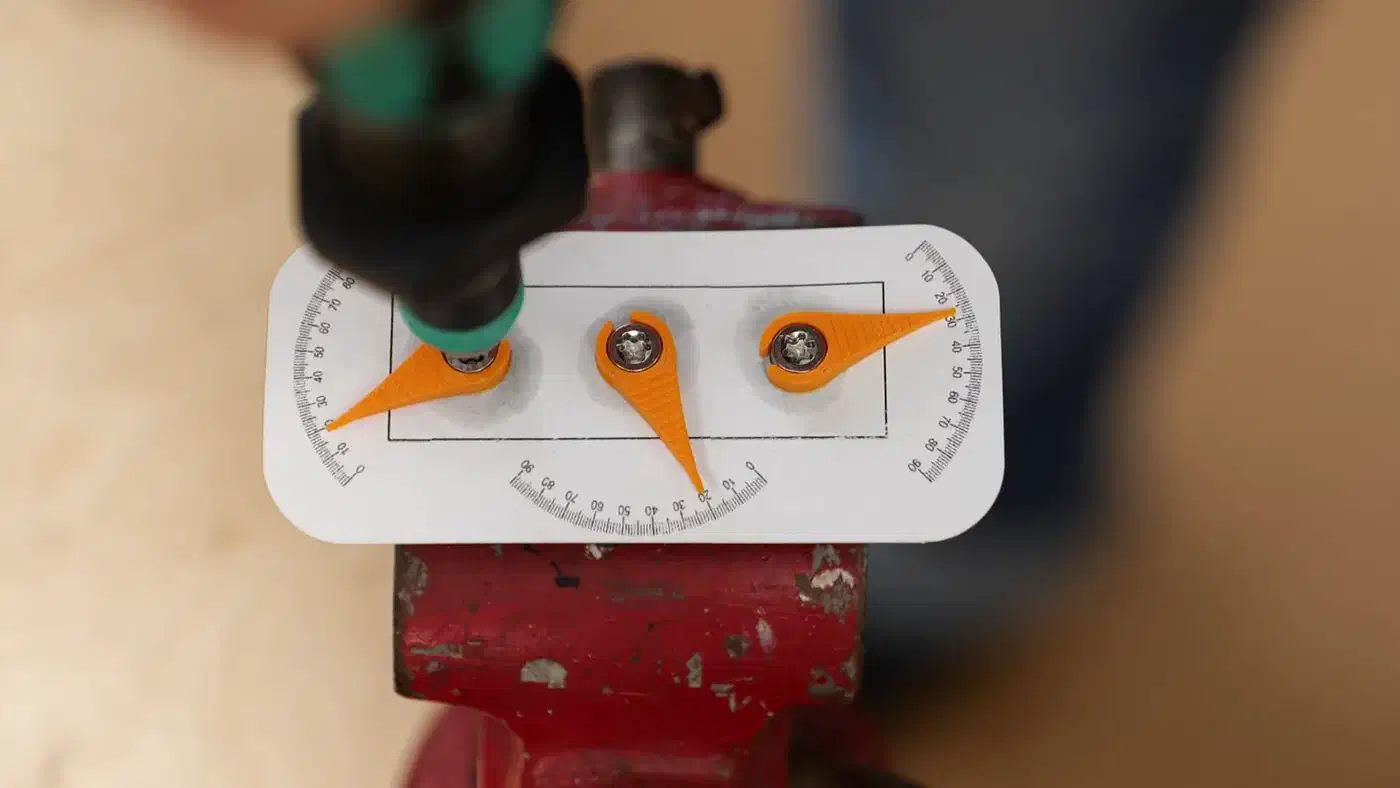
Stefan Hermann ran the test because of his own printer.
a few years later I printed a VORON 0 from the same carbon fiber reinforced nylon, which was a huge mistake because I quickly realized that my prints deformed over time, requiring me to tighten all the screws basically every day because the material flowed away under the constant load
Annealing fixed it. Eight hours at 110°C brought PA6-CF creep down to the level of ordinary polymers: two slight re-torques across the week instead of daily.
In the spring test, loaded to only 25% of tensile strength, annealed PA6-CF showed the lowest creep of all four nylon samples. Annealing PA12-CF changed almost nothing.
Carbon fiber is what makes annealing usable. PLA warps over 10% in the oven. The PA6 and PA12 bars deformed under 0.5%, invisible on a normal part.
What your printer needs to run either filament
Both filaments ask for the same hardware. Plan on about 280°C at the nozzle and a hardened steel nozzle, because the fibers chew through brass fast.
Dry the spool before printing. Twenty hours at 80°C cleared both grades in the test. PA6 needs it most, since 3% water on a 1 kg spool is close to a shot glass of moisture.
Bed adhesion was easy. PEI sheets with a thin coat of nano polymer adhesive held every print, leaving a slightly rough, shiny finish.
An enclosed, heated chamber helps layer adhesion and trims warping. Still, both filaments printed cleanly on an open machine, because the fibers stop the lifting on their own.
Annealing needs an oven or dryer that reaches 110°C, which rules out most filament dryers topping out at 65 to 80°C.
Parts start dry and drift wet. For predictable numbers, condition them on purpose instead of being surprised a month later.
Which carbon-fiber nylon should you print?
Pick PA6-CF when you need the most heat resistance, up to about 205°C, the most toughness, or the lowest cost per spool, and you will run the anneal cycle.
Pick PA12-CF when you want parts that behave in six months the way they behaved on day one. It is the low-maintenance choice, at a slightly higher price.
Skip both for a part under constant load in a humid room. Fiber-reinforced ASA or polycarbonate holds its numbers better, because they barely notice moisture. Bambu’s PPA-CF is another nylon option, losing under 3% of its strength when humid.
The builder whose printer started this landed in the same place. Even knowing to anneal, he would not print another VORON 0 in carbon-fiber nylon, because the stiffness he wanted is gone once the parts saturate with water.
Good homes remain for PA6-CF: cooling shrouds, hot-side brackets, anything where 205°C headroom and impact toughness beat raw stiffness.
| Property | PA6-CF | PA12-CF |
|---|---|---|
| Water uptake | up to 3% | up to 0.5% |
| Dry tensile strength | 140 MPa | ~120 MPa |
| Strength kept after conditioning | 56% | ~85% |
| Dry bending deflection, same load | 0.7 mm | 1.15 mm |
| Failure temperature | 205°C | 170°C |
| Creep under load | high unless annealed | low |
| Relative price | lower | higher |
Print PA6-CF when you want peak stiffness and heat and will keep the parts dry and annealed, and print PA12-CF when you want steady numbers with no fuss. Where the part will live counts for more than the dry spec sheet.