ASA keeps 80 percent of its impact strength under UV light
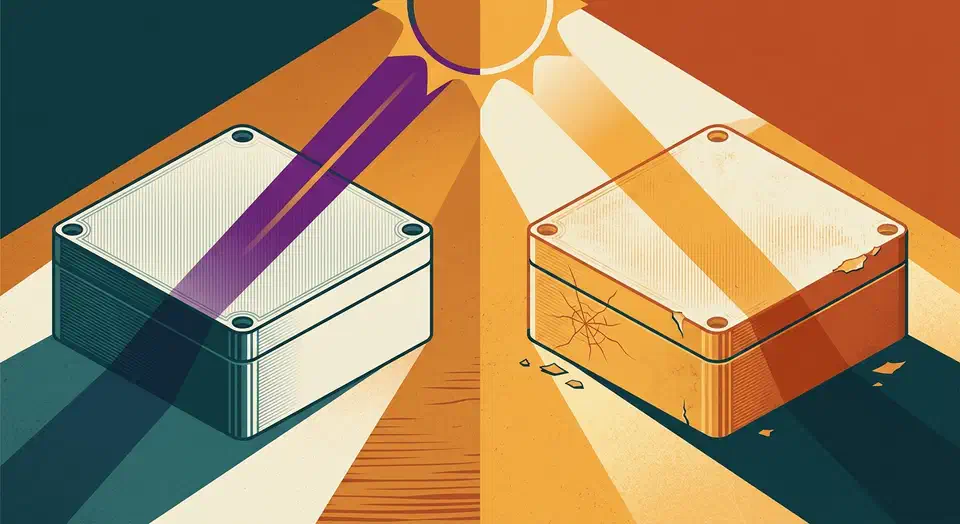
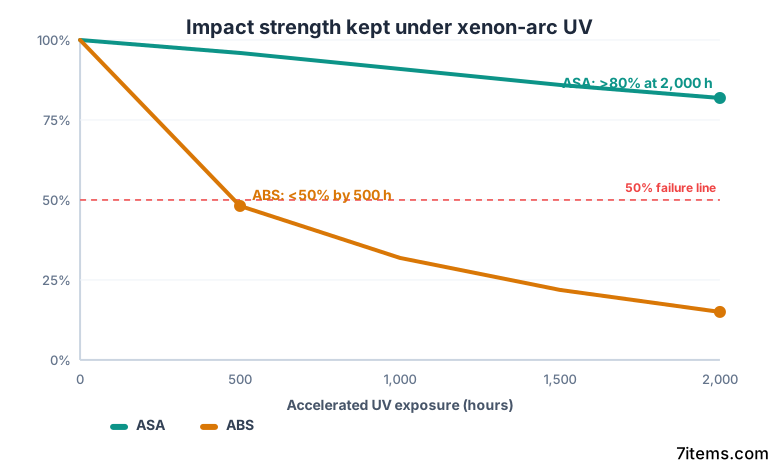
In the ASA vs ABS matchup under sunlight, ASA wins by a wide margin. Under the same xenon-arc UV test, ASA keeps over 80% of its impact strength at 2,000 hours, while ABS falls below 50% inside 500 hours. Their strength and stiffness nearly match. Where they part ways is finishing, because ABS smooths in acetone and ASA does not.
Key Takeaways
- ASA keeps over 80% of its punch after 2,000 hours of UV testing.
- ABS loses more than half its impact strength in under 500 hours.
- On strength, stiffness and heat, the two are basically a tie.
- ABS smooths glassy in an acetone bath, but ASA needs sanding and priming.
- ASA prints about 10°C hotter, so check your hotend can hold 260°C.
What makes ASA resist UV when ABS does not?
Both plastics use almost the same recipe. Each is a hard base plastic mixed with a soft rubber to make it tough, and they differ in the rubber.
ABS uses a rubber called polybutadiene. It carries weak chemical bonds that soak up UV light. The light then snaps the plastic chains apart. You see it as chalking, yellowing, cracking and lost impact strength, as LayerX3D’s ASA vs ABS guide lays out.
ASA swaps in an acrylic rubber that lacks those weak bonds. With no easy target for sunlight to grab, it breaks down far more slowly. 3DXTech makes the same point from the filament maker’s side.
Chemists developed ASA on purpose to fix this weak spot in ABS.
How much impact strength does each material keep under UV?
Under accelerated xenon-arc UV testing, ASA keeps more than 80% of its impact strength at 2,000 hours. ABS usually drops below 50% inside 500 hours under the same test.
Color shifts more slowly. ASA stays under dE 3 after five years outside, while ABS yellows within three to six months. A dE 3 shift is a color change most people would not spot with the two parts side by side.
These are sped-up lab hours rather than calendar hours. They rank materials against each other well, but they do not turn into years on a roof. Intertek’s xenon-arc exposure lab states that no direct correlation can be made between accelerated weathering time and actual outdoor exposure time.
The 80% figure comes from broad lab testing rather than one named spool, so it describes ASA in general, and any single reel may land above or below it.
Outdoors, an ABS part fades first, then cracks the first time something knocks it.
ASA vs ABS mechanical properties compared
On the bench, the two materials read almost identically across every static property.
| Property | ASA (FDM) | ABS (FDM) |
|---|---|---|
| Tensile strength | 28-34 MPa | 27-38 MPa |
| Flexural modulus | 1,800-2,100 MPa | 1,900-2,200 MPa |
| Notched impact (Charpy) | 18-22 kJ/m² | 15-20 kJ/m² |
| Impact (Izod, 3DXTech grade) | ~321 J/m | ~200-400 J/m |
| Heat deflection temp. | 95-100°C | 88-98°C |
| UV resistance | >80% at 2,000 h | <50% at 500 h |
| Color stability (outdoor) | <dE 3 at 5 years | Yellows at 3-6 months |
The Izod row uses J/m and the Charpy row uses kJ/m², two different tests run on different specimens, so one can’t be converted into the other. The same geometry gives you about the same stiffness and strength in either material, and the difference shows up only after time in sunlight.
Print settings: ASA runs about 10°C hotter than ABS
ABS wants roughly 230-250°C at the nozzle with a 100-110°C bed. ASA wants roughly 240-260°C at the nozzle with a 90-110°C bed.
That gap is the one hardware check to make before you buy. Your hotend has to hold 260°C for the length of a print, and many stock hotends sag at that temperature over a long job.
Both materials warp hard on open-frame printers and want a sealed chamber warmed to about 45-55°C. Without one, the layers split apart and the print fails. Keep part cooling low or off for ASA, because too much cooling weakens the bond between layers. Bambu’s X2D goes further and heats its chamber to 65°C with a dedicated heater.
ABS carries the warping reputation, yet 3DXTech reports ASA is often the easier of the two on a well-tuned machine. Plenty of users run it open-frame on a heated bed with the fan off. ASA also flows a touch thicker, which can help bridges sag less, though the gap is small enough to lose in normal print-to-print swings.
Both give off styrene and acrylonitrile fumes while printing, so run either in a sealed printer with a carbon filter or a vent, and never in a closed room. And if you print ASA-CF, the carbon-fiber grade, you must use a hardened steel nozzle. The gritty fill chews through brass inside a single spool.
The acetone problem: what you give up by switching to ASA
ABS dissolves in acetone, and that is what makes vapor smoothing work. A quick acetone bath gets a printed ABS part close to an injection-molded finish.
ASA does not dissolve in acetone. The same rubber that buys the UV resistance also shrugs off solvents, so the easy vapor route is gone. The standard ASA path to a smooth face is by hand: sand from 120 grit up through 400-600 grit, then prime before you paint. It is slow work, and you can’t leave it to soak the way you can with ABS.
ASA does respond to a stronger solvent called MEK, which Alliance Chemical documents as an ASA and ABS finishing solvent. MEK is far more toxic and flammable than acetone. It needs a fume hood and spark-safe gear, so it is out of reach for most home setups.
For paint, both take car acrylic lacquer, polyurethane and two-part epoxy after a light scuff with 320 grit. For outdoor ASA, add a UV-rated topcoat, because the paint fades even when the plastic under it does not.
ABS cement is just ABS melted in solvent, so it grips ABS but does nothing on ASA. Super glue and methylene-chloride cements grip both, and two-part epoxy is the pick for joints that carry weight. On price, ASA runs about 20-35% more per kilogram than plain ABS at the same quality tier. That is tiny on a one-off part, but it shows up once you pass about 50 parts.
Which should you print, ASA or ABS?
If the part sees sunlight in service, print ASA. If it does not, ABS is the cheaper and easier choice. A widely stocked outdoor option is Polymaker PolyLite ASA, and commodity ABS covers the indoor side for less.
Reach for ASA on parts that live outside:
- Outdoor enclosures, sensor housings and rooftop electronics boxes
- Automotive exterior trim and mirror covers
- Drone airframes and mounting hardware
- Signage brackets, garden fittings and utility meter covers
Reach for ABS when the part stays indoors or needs an acetone-smooth face:
- Indoor jigs and fixtures
- Consumer electronics housings
- Tooling mock-ups and master patterns for silicone molds
Step up to ASA-CF when you need UV resistance plus extra stiffness, for a structural outdoor bracket or a drone airframe. Budget a hardened nozzle with it. If you need more heat resistance than ASA’s 95-100°C limit, neither answer fits, and you are into polycarbonate, PEI or PEEK territory.